Deep dive · not in the main menu
Six stations, in the order a tote meets them.
01 / STATIONS
Zone C, bay by bay
The whole cycle
Station 01
Ambient · 90 seconds
Pre-rinse
A high-volume, low-pressure ambient flush. The goal is mass removal, not cleaning. Every pound of residue carried off here is a pound that does not consume caustic later, and caustic consumption is the biggest variable cost on the line. The effluent goes straight to the settling tank at the head of the reclaim skid.
Station 02
130–150 °F · 4–14 minutes
Caustic soak
Sodium hydroxide solution at a concentration set by prior-cargo class, held at temperature in a jacketed tank. Dwell time is the dial we turn: four minutes for a water-based ag-chem, fourteen for a cured resin residue. Every batch is logged with concentration, temperature, start time and operator initials. That log is what becomes your wash record.
Station 03
130 °F · 3 minutes
Internal agitation
A rotating spray head drops through the 6 inch port and drives a fan jet against the bottle wall through a full rotation. This is where the corners and the dome actually get cleaned — a static fill-and-drain soak never reaches them properly, which is the single most common weakness in home-built wash setups.
Station 04
150 °F · 2 minutes
Hot rinse
Two passes. The first uses reclaimed water from the carbon-polish stage of the skid; the second is a fresh-water polish that guarantees the final surface sees clean water. Splitting the rinse this way is what lets us hold 86% reclaim without compromising the finish.
Station 05
Warm air · 8–20 minutes
Dry
An air knife over the port, then dwell on the rack. Residual moisture in a sealed HDPE bottle is how mould and odour start, and it is the most common fault in units washed by people in a hurry. We would rather hold a rack an extra ten minutes than ship a damp tote.
Station 06
— · 4–6 minutes
Dry-and-sniff, grade, test
A human opens the lid and smells it. There is no instrument on the market that beats a trained nose for detecting fixed odour in HDPE at the levels that matter. Then nineteen inspection points at the grading bench, a leak test, and a UN re-mark for eligible units.
02 / WATER
The reclaim skid is the whole trick
Without water reclaim, a wash line is an environmental liability pretending to be a solution. Ours has three stages. A settling tank drops out solids and heavy residue by gravity over a twelve-hour cycle. Bag filtration takes out the suspended fraction in two passes, coarse then fine. A carbon polish stage handles dissolved organics and, more importantly, odour.
The output is clean enough for station four's first rinse pass but not for the final polish, which is why we split the rinse. That design decision is the difference between 86% reclaim and the roughly 60% most lines manage.
What we got wrong
The 2017 skid was sized for the throughput we had rather than the throughput we wanted, and we replaced the entire filtration stage eighteen months later. If you are building one: size for triple your current volume. The incremental cost at build time is small. The retrofit cost is not.
Skid specification
- Stage 1Settling, 12 hr residence
- Stage 2Bag filtration, coarse + fine
- Stage 3Granular activated carbon
- Reclaim rate86% of line draw
- Fresh water per cycle≈1.5 gal
- Sludge handlingDewatered, licensed disposal
- Built / rebuilt2017 / 2019
Cargo classes and dwell
- Water-based ag-chem4 min
- Detergents, surfactants8 min
- Food syrups and oils6 min
- Latex and adhesives12 min
- Cured resin residue14 min + rework
- Unknown (quarantine)Not washed
A / SPECIFICATION
Reference
Dimensions, fittings and seat materials
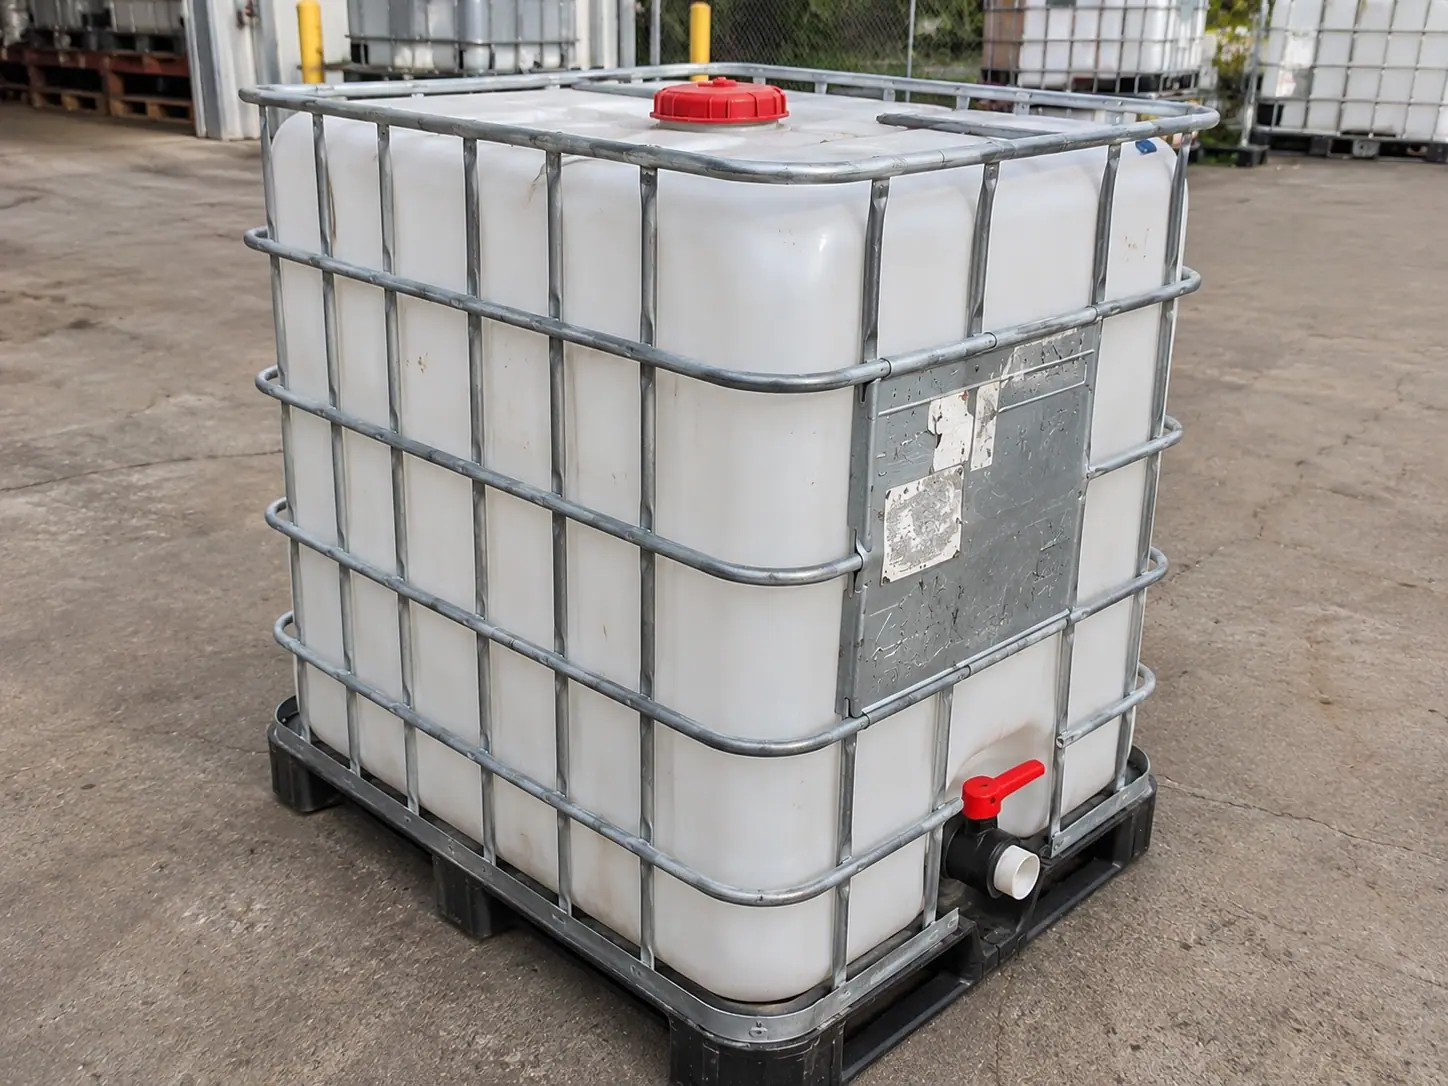 Fig. 1
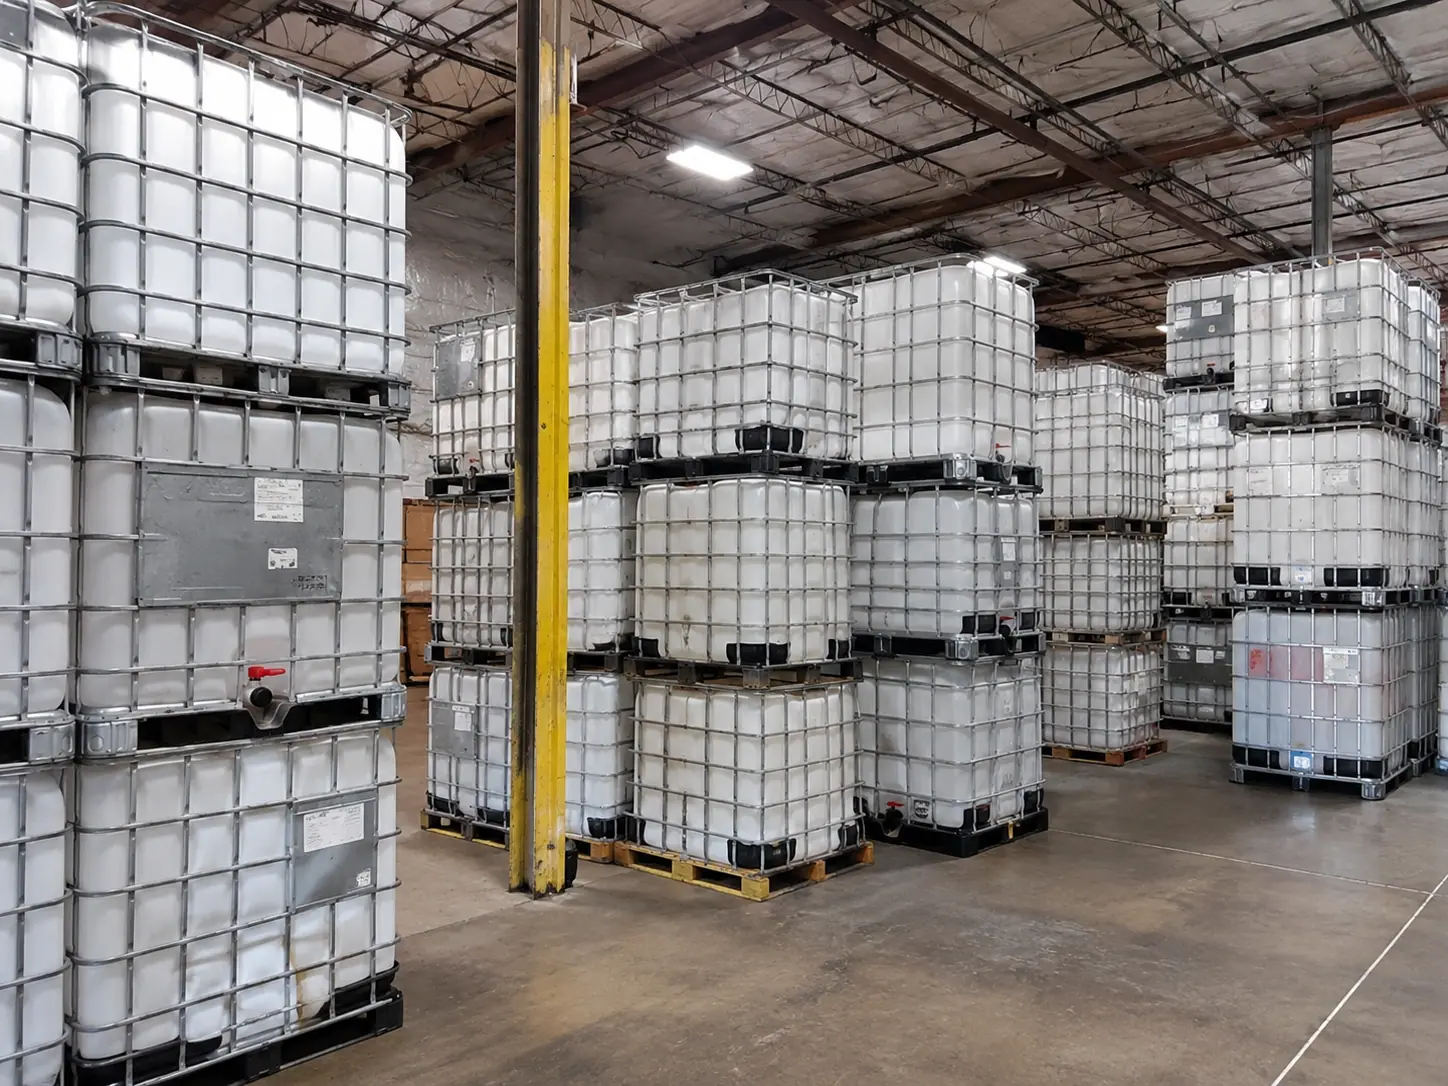 Fig. 2
| Capacity | Litres | Footprint | Height | Tare | Gross (water) | Stack loaded |
|---|---|---|---|---|---|---|
| 275 gal | 1,041 | 48 × 40 in | 46 in | ≈140 lb | ≈2,435 lb | 2 high |
| 330 gal | 1,249 | 48 × 40 in | 53 in | ≈155 lb | ≈2,905 lb | 2 high |
| 350 gal | 1,325 | 48 × 40 in | 56 in | ≈165 lb | ≈3,075 lb | 2 high |
| 120 gal | 454 | 40 × 32 in | 38 in | ≈95 lb | ≈1,095 lb | 2 high |
| 180 gal | 681 | 42 × 36 in | 42 in | ≈115 lb | ≈1,616 lb | 2 high |
| 550 gal | 2,082 | 60 × 48 in | 60 in | ≈240 lb | ≈4,830 lb | 1 high |
B / FITTINGS
What threads onto it
Fittings, threads and seat materials
| Fitting | Size | Seals by | Seat options | Typical service |
|---|---|---|---|---|
| S60x6 butterfly valve | 2 in | Flat gasket face | EPDM, Viton, PTFE | The standard IBC outlet |
| S70x6 butterfly valve | 2 in | Flat gasket face | EPDM, Viton | European and some 330 gal units |
| 2 in NPT ball valve, poly | 2 in | Thread flanks + tape | EPDM, Viton | Retrofits, metered dispensing |
| 2 in NPT ball valve, stainless | 2 in | Thread flanks + tape | PTFE | Solvents, pressure, hot cargo |
| 3 in butterfly valve | 3 in | Flat gasket face | EPDM, Viton | Viscous cargo, high flow |
| 6 in fill cap | 6 in | Gasketed lid | EPDM, silicone | Vented or solid — choose deliberately |
| Camlock adapter, type C | 1.5 / 2 in | Cam arms + gasket | Buna, Viton | Repeated connect / disconnect |
| Bulkhead tap | 3/4 in | Both-side gaskets | Brass, poly | Rain kits, site water |
| Material | Good with | Avoid with | Temperature | Cost |
|---|---|---|---|---|
| EPDM | Water, acids, caustics, brine, ag-chem | Oils, fuels, aromatics | -40 to 250 °F | Low |
| Viton (FKM) | Solvents, oils, fuels, aromatics | Ketones, amines, hot steam | -15 to 400 °F | High |
| Nitrile (NBR) | Oils, diesel, greases, hydraulics | Ozone, strong oxidisers | -30 to 250 °F | Low |
| PTFE envelope | Almost all chemistry, high purity | Needs very flat flange faces | -100 to 450 °F | High |
| Silicone | Food contact, wide temperature | Solvents, abrasion | -60 to 450 °F | Medium |
E / GRADING
A grade is a promise, not a mood
How every unit is scored
| # | Point | Critical? |
|---|---|---|
| 01 | Prior cargo declaration — present, written, specific | Yes |
| 02 | Residual liquid — any volume at all | Yes |
| 03 | Odour after wash — fixed odour by trained nose | Yes |
| 04 | Bottle corner stress whitening | No |
| 05 | Interior scoring you can feel | No |
| 06 | Interior crazing — fine surface cracking | Yes |
| 07 | Bottle bulge or deformation | Yes |
| 08 | Wall thickness at the thinnest point | Yes |
| 09 | Dome port condition and flange flatness | No |
| 10 | Outlet threads — cross-threading, chipping | Yes if crossed |
| 11 | Valve function, full open and close | No, replaceable |
| 12 | Gasket condition — compression set, bloom | No, replaceable |
| 13 | Cage squareness along the top rail | No, pressable |
| 14 | Cage weld integrity at tube intersections | Yes |
| 15 | Cage coating and galvanising loss | No |
| 16 | Pallet condition — cracked feet, rot, corrosion | No, replaceable |
| 17 | Forklift pocket integrity | No |
| 18 | UN marking legibility and date | No, re-markable |
| 19 | Leak test under our procedure | Yes |
D / ORDERING
Commercial terms, up front
Lead times, minimums and what happens when it goes wrong
| Item | Detail |
|---|---|
| Minimum order | One unit. No account minimum, no membership. |
| Stock lead time | Grade A and B 275 gal usually ship the same week |
| Rebottled lead time | 2–3 weeks, built to order in bay D |
| Food-grade lead time | 1–3 weeks when stock exists; supply-dependent |
| Full truckload | 45 on a 48 ft flat, 48 in a 53 ft van, 90 empties double-stacked |
| Payment, first order | Prepay by ACH or card |
| Payment, established | Net 30 on credit approval |
| Grade guarantee | Regrade or replace, our freight both ways, 14 days |
| Leak warranty | 30 days from delivery, normal atmospheric service |
| Cancellation | Free until the truck is loaded |
| Returns | 14 days on unused stock units, freight at your cost |
| Sales tax | Indiana resale certificates and out-of-state equivalents accepted |
G / PITFALLS
Learned the expensive way
Five mistakes that cost people money
Ordering a 330 without measuring the ceiling
A 275 and a 330 share a footprint; the 330 is seven inches taller. Two 330s stacked is 110 inches against 96 for two 275s, and most sprinkler regimes want eighteen inches of clearance below the deflector. That seven inches is frequently the whole margin.
Forcing an NPT fitting into an S60x6 port
Both are roughly two inches, so it bites and feels tight. It is not sealing, it is chewing the buttress thread. The joint weeps two days later, usually in transit, and cross-threading is one of the few faults that condemns an otherwise perfect bottle.
Reusing a flange gasket
A gasket is a one-use part the moment it has taken a compression set. Reusing one is the cause of most 'the new valve still leaks' emails we get. They cost a couple of dollars. Keep a box at the fill point.
Specifying a solid lid on a tote that sees sun
Sealed container, rising temperature, nowhere for the expansion to go. The bottle bulges between the cage bars and does not fully return. A vented lid is the cheapest risk control in this industry.
Ignoring specific gravity
A full 275 of water is 2,435 lb. The same tote of UAN 32 is 3,168 lb, and a 330 is 3,785 lb. Plenty of lift-gates are rated at 2,500 or 3,000 lb, and the rating assumes a centred load.
F / END OF LIFE
Reuse first, recycle last
What happens when the container is finally finished
| Step | Outcome | Share of mass | Cost to us |
|---|---|---|---|
| 01 | Reuse as is — wash and redeploy | 63.9% | 11 gal of mostly reclaimed water |
| 02 | Repair and reuse — valve, gasket, pallet, cage | 11.4% | Parts and bench time |
| 03 | Rebottle — new bottle, reclaimed steel | 9.6% | A new bottle, two thirds of mass retained |
| 04 | Upcycle — rain kits, grow beds, wash stations | 3.2% | Fabrication time |
| 05 | Material recovery — HDPE regrind, steel, wood | 11.3% | Grinding, washing, drying energy |
| 06 | Residual to licensed disposal | 0.6% | Sludge, gasket rubber, fasteners, laminates |
Operator to operator